Stanton, Orange County
Factory Locksmith Service for Stanton Manufacturers
Short answer: Safety comes first on a plant floor. A factory locksmith can cut keys for machine selector switches and fit locks to guarded cabinets, but never bypasses interlocks, e-stops or lockout/tagout devices. We also follow your PPE and escort rules. In Stanton, we work every day, 6:30 a.m. to 11:30 p.m. We're closed overnight.
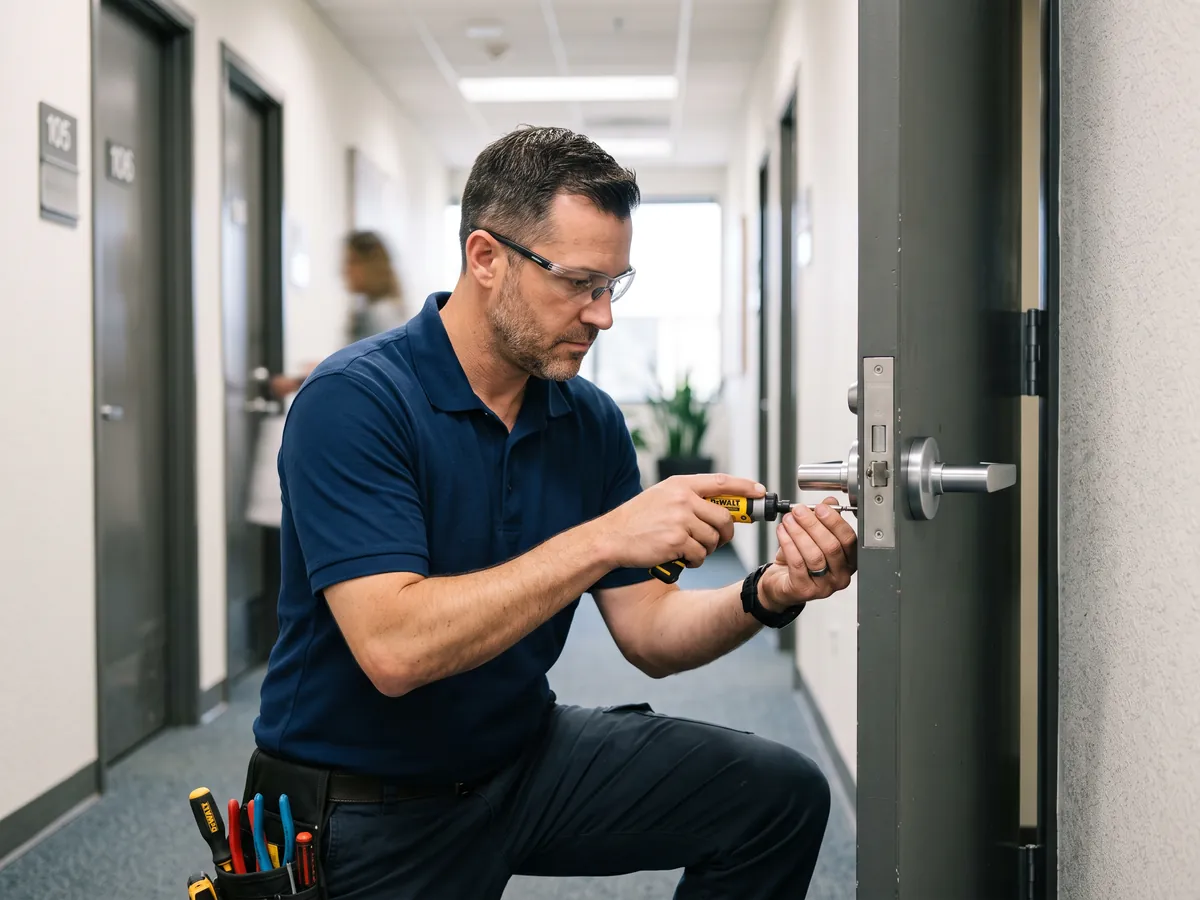
Locksmith work and machine safety overlap in only a few places, and it helps to know where. In Stanton, Julian's Locksmith cuts and rekeys keys for selector switches, guarded cabinets and tool cribs. We do not bypass interlocks, defeat guards, or touch lockout/tagout programs; those belong to your safety lead and your electricians. Equally, we won't alter hardware in classified hazardous locations unless your engineer confirms the part is rated for it. What we can do is make the keys and locks around that equipment organized and accountable. When your question sits on the boundary, a factory locksmith should say so up front, then help you work out who at your plant needs to answer it.
Factory Locksmith in Stanton: what to expect
Most factories already have a key system; it just wasn't designed. Three shifts mean three sets of opening and closing duties. Maintenance needs the electrical rooms but not the lab. Quality needs the lab but not the stock cage. Contractors need the roof hatch for a day. An interchangeable core system answers this well: the lock body stays in the door, and the core, which carries the keyway, can be swapped with a control key in seconds. When a key goes missing, you replace one core, not the lock. Pair that with a restricted keyway so copies can't be made at a kiosk, and a key log that records every issue and return. For areas with an audit need, a card or keypad reader records entries and lets you cancel a person's access immediately. A factory locksmith explains the options and costs, then helps you put each area on the layer it deserves. Cores add cost up front but save rekeying labor later.
What we can do on-site
- Key control audit and plant-wide rekey. Before a factory locksmith changes a single cylinder, we audit who needs access to what. We walk the plant with your maintenance or safety lead, list every keyed opening, group them by department and shift, and flag the ones with lost or unaccounted keys. The result is a short plan: what to rekey now, what to leave and what to add.
- Tool crib, maintenance shop and stockroom locks. Tool cribs hold expensive, portable property, and the lock on the door is only half the story. We fit Dutch doors and service windows with deadlatching hardware, set keying so only crib attendants hold keys, and add a keypad or card reader if you want a record of who enters after hours.
- Electrical room and control cabinet locks. Electrical rooms and motor control centers should be reachable only by qualified people. We rekey them to a restricted keyway, add a deadlatching lock where the door has none, and make sure the door still opens from inside without a key, because anyone working in the room needs a way out.
- Chemical, solvent and flammable storage locks. Hazardous-material rooms invite tampering by curious hands, not just thieves. A deadlatched door with a restricted key, a clear sign-out record and a closer that returns the door to latched every time prevents most of it. We set those up and leave the chemical rules to your safety coordinator. A lock your crew will actually use beats one they prop open.
- Exit devices and egress hardware on the floor. Production floors need dependable exit devices, because crowds, forklifts and heavy carts all work against them. We install and repair rim, vertical rod and concealed rod devices from Von Duprin, Detex and Sargent, adjust latch height and strike alignment, and replace worn parts before a door fails to release. Line workers rely on these devices daily, so reliability matters more than looks.
What's different about Stanton
Older neighborhoods in Stanton sometimes hold small factories in converted brick buildings, former garages or mid-century industrial blocks. Their doors may have cast-iron mortise locks, wood frames or hardware no longer sold. A factory locksmith there repairs original pieces where possible and fits modern cylinders into old mortise bodies, so the building keeps its character and gains key control. Brass and bronze originals are worth keeping when the bolt and case are still sound.
Industrial areas around Stanton mix factories, warehouses and truck yards in the same park, so a plant's perimeter is often shared with logistics tenants. A factory locksmith there helps separate the plant's keyway from the neighbors', secures shared truck courts, and treats the dock man door as part of the production perimeter, not an afterthought. We also keep each tenant's keys separate, since shared yards invite finger-pointing when something goes missing.
Many plant workers in Stanton drive in on Western Avenue for early starts, and a lost key before sunrise can hold up a whole line. Our day begins at 6:30 a.m., which covers first-shift problems quickly. Our factory locksmith service suggests a spare ring with a supervisor who lives close and a documented backup, so one missed key doesn't delay production. Planned work can also be timed for the lull after the first break.
Common situations
- A plant moves into a new building in Stanton and brings its old locks along. Half the doors in the new space have unknown keys from earlier tenants. We'd rekey the space before move-in, set up the same layered system that worked at the old plant, and give the manager a map of doors to keys so the move doesn't begin with a lockout. Door labels that match the key chart make the first week much smoother.
- Consider a metal fabricator whose scrap yard loses copper off-cuts every month. The yard gate chain is loose, and the bin padlocks are all the same cheap model. We'd fit shrouded padlocks on heavy hasps keyed to one restricted system, and suggest a motion light on the yard side facing Chapman Avenue so anyone prowling there is visible from the street. Thieves tend to test the weakest padlock first, so every bin gets the same hardware.
- On a Thursday afternoon, a plant manager realizes the control key for the interchangeable cores is missing, and a shift lead needs a core swapped tonight. We'd confirm authority by phone and, if the system is one we installed, bring what's needed and finish well before 11:30 p.m. If it isn't ours, we'd explain what the core manufacturer requires. Either way, we'd recommend a second control key held by a named backup.
- For example, the electrical room door near the compressor jams at the start of second shift, and a maintenance tech can't reach a breaker panel. We'd arrive, meet the safety escort, find that vibration has shifted the strike and latch, and re-secure the hardware with thread-locking compound, leaving the door secure and openable from inside. We'd also check the other doors along that wall, since vibration rarely affects only one.
How the visit works
- Call and describe your plant. Call (951) 903-3193 and tell us the address, what the plant makes, how many shifts run, and what you need: a rekey, a repair or a key system. Mention any hazards, PPE rules or sign-in steps so we arrive prepared. A phone photo of any damaged lock is worth a paragraph of description.
- Complete safety orientation and sign-in. If your site requires a safety video, a contractor permit or a hot-work or confined-space briefing, tell us before the visit. Locksmith work doesn't normally involve those hazards, but we won't skip an orientation your rules require. Most orientations are short, and we're glad to complete them before work starts.
- Verify authority and walk the areas. Hazardous or restricted rooms get special attention. We confirm with your escort what we can enter, what needs a permit and which doors must not be left unlatched while we work. If a room is classified, we stop and ask for your engineer's guidance.
- Quote the plan in writing. Where a system is involved, such as cores or restricted keys, the quote also explains how it will work: who holds the control key, who may request copies and what a lost key costs to fix. You see the rules before you commit.
- Do the work around production. Our hours are 6:30 a.m. to 11:30 p.m., every day of the week. We're closed overnight. If your plant runs weekend shifts, we finish key work earlier in the week so those crews begin with the new system.
- Test, document and train. Each lock is tested with its new key, from both sides where it applies. We check that exits still release without a key, and that doors latch under the closer. Then we hand over the keys and the key chart. Any key that doesn't test perfectly is recut on the spot.
What affects the cost
- Hardware grade, cores and keyway. Interchangeable cores cost more per door than standard cylinders but save labor later. We compare the up-front cost against the expected number of key changes, so you only buy cores where turnover justifies them. We'll show the savings math so the decision isn't based on a sales pitch.
- Production constraints. If the work needs a planned shutdown, a permit or a second trade, that time is part of the job. We tell you in the quote what the plant must provide, such as an escort, a lockout of nearby equipment or a cleared aisle.
- Condition of doors, frames and equipment. Heavy wear raises the bill. Cylinders packed with swarf, seized latches and corroded hasps often need replacement, not cleaning. When an old part is still available, we try to repair it; when it isn't, we quote a modern replacement. We photograph what we find, so your maintenance records show why a part was replaced.
Every job gets a clear quote before any work starts. Call (951) 903-3193 with the details and we'll tell you what to expect for your situation in Stanton.
Advice before you book
- Test exit devices on a set day, such as the first Monday of the month, and log the date. A device should release with one hand and no hesitation. A log shows an inspector that you check, and a stiff device gets repaired before it fails.
- Walk your plant with a clipboard and list every keyed opening: doors, cabinets, cages, gates, key switches. Note who has keys to each. That one-page inventory is the starting point for any key system, and it often reveals doors nobody knew were locked. Hand a copy to your factory locksmith so quotes match what is really on the floor.
- Protect the outside as carefully as the inside. Yards, scrap bins and loading docks are where material leaves. A shrouded padlock on a through-bolted hasp, a motion light and a clear key list make theft harder than a rekeyed office door. A cheap padlock invites the first test.
- Ask your safety lead to be part of the lock project. They know the egress rules, the hazard classifications and the lockout program, and they can tell a factory locksmith before the visit which doors may never be chained or delayed. Their involvement prevents rework.
What not to do
- Chaining or dogging an exit shut to stop door use during shifts. It may save a few steps, but it blocks an emergency path and invites citations. Talk to a factory locksmith about alarmed or delayed-egress hardware where your fire marshal allows it.
- Choosing hardware for the catalog photo, not the room. A brass lever looks fine until it meets washdown chemicals or metal dust. Tell your factory locksmith what the room is like and choose materials for it. Specify the finish when you order, and ask if you're unsure.
- Letting a vendor bypass a safety switch to save time. If a lock or switch is part of a machine's safety circuit, the fix is repair or replacement by the proper trade, not a jumper or a spare key left taped to the machine.
Service in Stanton
Stanton is about 55 miles from our San Bernardino base, roughly 60 minutes in light traffic via I-215 South through Colton and Grand Terrace to SR-91 West in Riverside, SR-91 West through Corona and Santa Ana Canyon to SR-57 South. When you call, you get an arrival estimate based on where the technician is and the traffic at that moment.
Most trips into Stanton use Magnolia Avenue for at least part of the drive, and the technician keeps an eye on live traffic along the way so the arrival estimate you heard on the phone stays honest.
About Stanton: Stanton named the jacaranda its city tree and the bird of paradise its city flower in October 1959 on the recommendation of the Stanton Women's Civic Club.
| Neighborhoods | Cedar Street, Hollenbeck Park area off Cerritos Avenue, Beach Boulevard corridor, Briarwood Street and Premier Park, Dotson Park area off Fern Avenue, Date Street |
|---|---|
| ZIP codes | 90680 |
| Main routes | Beach Boulevard, Katella Avenue, Western Avenue, Knott Avenue |
| From our San Bernardino base | about 55 miles via I-215 South through Colton and Grand Terrace to SR-91 West in Riverside, SR-91 West through Corona and Santa Ana Canyon to SR-57 South, then SR-22 West (Garden Grove Freeway) to Beach Boulevard (SR-39) north into Stanton; alternate is SR-91 West to the Beach Boulevard exit in Buena Park and south on Beach, or I-10 West to SR-57 South when the 91 is jammed |
Business lock or door work in Stanton?
Call (951) 903-3193 with the address, the doors or hardware involved and when the site is open. We'll quote the job before any work starts and book a time within our hours that suits your schedule.
Frequently asked questions
Which locks suit washdown or food-processing areas?
Stainless steel levers, sealed or gasketed cylinders and smooth, crevice-free finishes hold up best, because they resist corrosion and clean easily. Lubricants must be ones your sanitation program approves. We choose hardware by the room's cleaning chemicals and temperature, and we schedule installation in a sanitation window so product isn't exposed. Ask your factory locksmith about timing, since a washdown schedule can limit the work window.
Will you follow our safety rules and PPE requirements?
Yes. We expect to sign in, take any required orientation and wear the protective equipment your plant specifies. We arrive in safety footwear and glasses and carry hearing protection. Tell us ahead of time about any special requirements, such as permits, badges or restricted zones, so we aren't delayed at the gate. Plants that need more than that should say so when booking.
Our plant runs three shifts. Can you work nights and weekends?
We aren't a 24/7 service. Julian's Locksmith works every day from 6:30 a.m. to 11:30 p.m., weekends included. Most planned work fits first and second shift. For graveyard-shift problems, keep a spare ring with the shift lead and a lockbox, and call us when we open at 6:30 a.m.
Can you bypass or replace a machine's safety switch or interlock?
No. Interlocks, e-stops, guard switches and trapped-key systems are safety devices, and altering them is a job for your electricians and equipment maker, not a locksmith. We can cut or replace the plain mechanical key for a selector switch or cabinet lock, and we'll tell you if the part you describe is part of a safety circuit.
What does a factory locksmith do that a regular commercial locksmith doesn't?
A factory locksmith works around production. That means following your safety orientation and PPE rules, scheduling around changeovers, choosing hardware for dust, washdown, vibration or heat, and organizing key control across shifts. Julian's Locksmith serves Stanton plants with restricted keyways, interchangeable cores, tool crib and cabinet locks, and exit device repair, always quoting before work. Every quote is in writing, and you receive a chart of which key opens what.
What is the difference between lockout/tagout padlocks and security locks?
Lockout/tagout padlocks isolate machine energy during servicing, and under the lockout/tagout rules each authorized worker typically applies a personal lock and keeps its key. Security locks control who can enter an area. They shouldn't be mixed. We can supply padlock sets keyed to your program, but your safety coordinator decides how that program works. Ask your safety lead if you are unsure which program a lock belongs to.
How far is Stanton from your base?
Stanton is about 55 miles from our San Bernardino base, roughly 60 minutes in light traffic. Arrival time depends on traffic and on the job the technician is finishing, so we give you an estimate on the phone before you commit.
Related services in Stanton
- Commercial Locksmith in Stanton
- Industrial Locksmith in Stanton
- Warehouse Locksmith in Stanton
- Key Control System in Stanton
- Employee Key Control System in Stanton
- Restricted Key System in Stanton
- High Security Locksmith in Stanton
- Panic Bar Repair in Stanton
- Commercial Master Key System in Stanton
- Commercial Security Locks in Stanton
Factory Locksmith in nearby cities
- Factory Locksmith in Garden GroveOrange County
- Factory Locksmith in CypressOrange County
- Factory Locksmith in WestminsterOrange County
- Factory Locksmith in Buena ParkOrange County
- Factory Locksmith in Los AlamitosOrange County
- Factory Locksmith in La PalmaOrange County
- Factory Locksmith in Hawaiian GardensLos Angeles County
- Factory Locksmith in AnaheimOrange County