Mentone, San Bernardino County
Factory Locksmith Service for Mentone Manufacturers
Short answer: A factory locksmith secures the places a production plant actually needs controlled: tool cribs, electrical rooms, chemical storage, quality labs, shipping doors and exit hardware. In Mentone, Julian's Locksmith works around your running lines, follows your safety rules on the floor, quotes before starting and keeps keys organized across shifts. Call (951) 903-3193 with your plant's door count and hours.
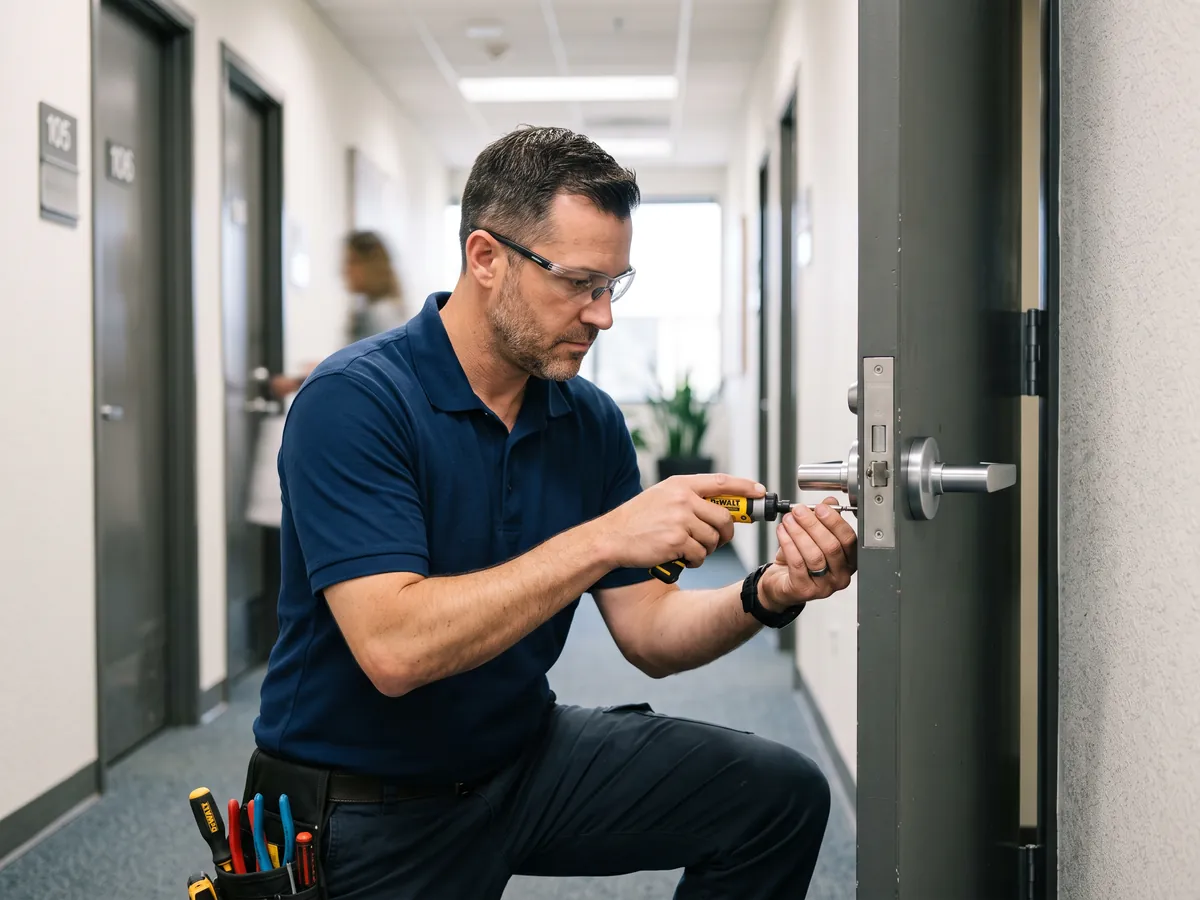
Nothing in a factory costs more than a stopped line, so a lock problem there is rarely only a lock problem. A tool crib that won't open delays a changeover, an electrical room door that's jammed holds up maintenance, and an exit device that sticks becomes a safety finding. A factory locksmith in Mentone has to think about production first and hardware second: when can the work happen, who escorts us, what must stay running, and which doors can be closed for an hour. Julian's Locksmith plans visits around your schedule, works quietly and quickly, and tells you plainly when a job needs a planned shutdown. Call (951) 903-3193 and tell us how your shifts run.
Factory Locksmith in Mentone: what to expect
A factory is governed by safety rules that a locksmith must respect. Exit routes have to open from the inside without keys, tools or special knowledge, which is the heart of OSHA's exit route standard and your local fire code. Lockout/tagout is another system entirely: the padlocks used to isolate machine energy are for safety, not security, and each authorized worker typically holds their own lock and key under the plant's written program. We can supply keyed-different or keyed-alike padlock sets if your safety program calls for them, but we never decide how that program works. Machine guards with interlock switches, trapped-key systems and e-stops are safety devices we leave alone. Where cabinet and selector keys are concerned, we cut and organize keys so the right people have them, nothing more. Working this way keeps a factory locksmith out of conflicts with your safety officer and keeps you out of trouble with an inspector.
Work included on a typical visit
- Key control audit and plant-wide rekey. A plant-wide rekey doesn't mean shutting down. We work department by department, resetting cylinders at changeovers or in quiet gaps, and test each key before moving on. Large plants are done across several visits so that no door sits open and no crew is left without access. A written schedule tells each supervisor which door changes on which day.
- Electrical room and control cabinet locks. Panel doors take vibration and heat. We re-secure latches with thread-locking compound, replace worn quarter-turn and three-point latches, and fit sealed cylinders where dust or spray is present. Work inside live cabinets stays with your electricians; we handle the lock, never the wiring. Ask your electrical lead which cabinets are safety-related before we replace any lock.
- Chemical, solvent and flammable storage locks. Hazardous-material rooms invite tampering by curious hands, not just thieves. A deadlatched door with a restricted key, a clear sign-out record and a closer that returns the door to latched every time prevents most of it. We set those up and leave the chemical rules to your safety coordinator. A lock your crew will actually use beats one they prop open.
- Shipping doors, scrap cages and material yards. Finished goods staged for pickup sit in a risky window between production and the carrier. A cage or locked bay with a restricted key and a short log closes that window cheaply. We build the cage hardware around how your shipping team actually moves product. A sign-out sheet at the cage door is often all the extra control a small plant needs.
- Machine keys, selector switches and padlock sets. Lockout/tagout programs use personal padlocks, usually keyed different for each worker, and in some plants a master held by a supervisor. We can supply padlock sets keyed to your program. Which devices and rules apply is your safety coordinator's decision; we supply the hardware. Whichever way the program is written, the key stays with the person whose lock it fits.
What's different about Mentone
Inland heat is hard on factory hardware. Metal-roofed buildings run hot, lubricants thin, plastic parts crack and batteries in keypads and fobs fade. In Mentone, a factory locksmith picks heat-tolerant finishes, schedules lubrication in spring, and checks that closers and latches still work when metal expands in July. Ovens, furnaces and boilers add local heat that standard hardware handles poorly. Heat-related drift is usually a quick adjustment, not a replacement.
Factories near the foothills handle wind-blown dust, brush fire smoke and the occasional evacuation order. Strong offshore winds slam doors that don't latch, and ash gums up cylinders. A factory locksmith adjusts doors to close firmly, chooses dust-resistant hardware and makes sure gates can still be opened by the fire department through a Knox key switch where required. After a smoky week, a quick cleaning of exposed cylinders is cheap insurance.
Many plant workers in Mentone drive in on I-10 for early starts, and a lost key before sunrise can hold up a whole line. Our day begins at 6:30 a.m., which covers first-shift problems quickly. Our factory locksmith service suggests a spare ring with a supervisor who lives close and a documented backup, so one missed key doesn't delay production. Planned work can also be timed for the lull after the first break.
Situations this covers
- Picture a machine shop where a tool crib attendant retires and the key to the crib door can't be found, while three machinists need tooling at once. We'd verify the owner's authority, open the cylinder, key a new one to a short list and add a sign-out sheet, so the next inventory count starts with a clean record. If the old keys turn up later, they will no longer work, which is the point.
- Imagine a food plant where washdown spray has corroded the lever on a processing room door. The sanitation lead wants something easy to clean. We'd propose a stainless lever with a sealed cylinder, discuss lubricant limits, and schedule the swap in the sanitation window so no product is exposed during the work. Old hardware goes out in a sealed bag so nothing carries into the room.
- Imagine a calibration lab in a small aerospace parts plant. The door has a standard office lock, and the lab holds gauges that can't easily be replaced. We'd swap it for a deadlatching Grade 1 lock on a restricted keyway, keyed to the quality manager and two technicians, and show the manager how to record who holds each key. The lab door also gets a closer so it can't be left ajar during a busy shift.
- Say a contract manufacturer wins work that requires controlled access to the prototype room, and the customer's requirements list who may enter. We'd install a Grade 1 lock on a restricted keyway, add a card reader through the plant's electrician, and hand over a key record that matches the customer's list for the quality manager to show an auditor. If the customer later changes the list, we'd rekey only the affected door.
From your call to the finished job
- Call and describe your plant. Have your safety or maintenance lead on the line if possible. They know where the restricted areas are, who escorts visitors and what training we need before entering. Ten minutes of detail on the phone saves an hour at the gate. We'll ask where our van can park without blocking a truck route.
- Complete safety orientation and sign-in. We stay in the areas assigned to us and keep tools out of walkways. If a machine is running near a door we need, we ask your escort to stop or reroute traffic first. We never reach into guarded equipment or touch controls that aren't ours.
- Verify authority and walk the areas. Before we change anything, we check ID and proof you can authorize work: a lease, a deed, a business license or a letter from the owner. Then we walk the plant with your lead, noting each door, cabinet and cage that is in scope.
- Quote the plan in writing. Where a system is involved, such as cores or restricted keys, the quote also explains how it will work: who holds the control key, who may request copies and what a lost key costs to fix. You see the rules before you commit.
- Do the work around production. We keep the work area tidy, collect metal shavings and old parts, and leave doors working as we found them or better. If something unexpected comes up, like a door frame too bent to hold a lock, we stop, explain it and requote before continuing.
- Test, document and train. Each lock is tested with its new key, from both sides where it applies. We check that exits still release without a key, and that doors latch under the closer. Then we hand over the keys and the key chart. Any key that doesn't test perfectly is recut on the spot.
What affects the cost
- Production constraints. Predictable access lowers cost. Giving us a single door to enter, a named escort and a time window means fewer delays than a vague come-whenever arrangement. It also makes it easier to plan around your shifts. Clear aisles and a door that's accessible when we arrive help too.
- Timing, drive and shift schedules. Planned work during our regular hours is the most economical. Calls near our 11:30 p.m. cutoff or on short notice cost differently because of scheduling and traffic. The quote is always stated before we leave San Bernardino. Ask for the earliest slot if you need work done before first shift starts.
- Electronic and compliance add-ons. Networked locks add software and sometimes subscriptions. For a plant with a few audited doors, the recurring cost may be worth it; for the whole building it may not. We lay out one-time and recurring costs side by side. Ask what happens to the system if the manufacturer changes its platform.
Every job gets a clear quote before any work starts. Call (951) 903-3193 with the details and we'll tell you what to expect for your situation in Mentone.
Practical tips before you call
- Walk your plant with a clipboard and list every keyed opening: doors, cabinets, cages, gates, key switches. Note who has keys to each. That one-page inventory is the starting point for any key system, and it often reveals doors nobody knew were locked. Hand a copy to your factory locksmith so quotes match what is really on the floor.
- Check doors after any equipment move or installation. New machinery, rerouted forklift paths and shifted racking change how doors swing and where they get hit. A quick look at latches and strikes after a layout change catches problems early. Include door hardware in the post-move walk-through your team already does.
- Think about what happens when power fails. Electric locks must be fail-safe or fail-secure according to the door's role, and exit doors must still release. When you add keypads or magnetic locks, ask which way the lock fails and whether a mechanical override exists.
- Give visitors and contractors a key procedure, not a loan from the supply room. A sign-out slip with a return time and a restricted key that opens only the needed door limits risk without slowing the work. Ask for the key back before you release the badge or the contractor's final payment.
What not to do
- Letting a vendor bypass a safety switch to save time. If a lock or switch is part of a machine's safety circuit, the fix is repair or replacement by the proper trade, not a jumper or a spare key left taped to the machine.
- Chaining or dogging an exit shut to stop door use during shifts. It may save a few steps, but it blocks an emergency path and invites citations. Talk to a factory locksmith about alarmed or delayed-egress hardware where your fire marshal allows it.
- Waiting for a lost key to turn into a shutdown. When the only key to an electrical room or tool crib disappears, the delay can ripple through a shift. Keep a spare in a controlled cabinet and a locksmith's number handy.
Service in Mentone
Mentone is about 20 miles from our San Bernardino base, roughly 27 minutes in light traffic via I-215 South to SR-210 East through Highland, exit San Bernardino Avenue in Redlands. When you call, you get an arrival estimate based on where the technician is and the traffic at that moment.
Homes and businesses just off Crafton Avenue are routine stops for us. Give the suite or unit number and any gate instructions, and say whether the van can park out front or should pull into a side lot.
About Mentone: The Mentone Hotel opened in 1892 as an inland beach resort, later became a sanitarium and closed in 1917, and residents still informally call the town Mentone Beach.
| Neighborhoods | Greenspot, Mill Creek Road, Capri, Original Mentone townsite, Mentone Boulevard corridor, Sandstone tract |
|---|---|
| ZIP codes | 92359 |
| Main routes | SR-38, SR-210, I-10, Lugonia Avenue |
| From our San Bernardino base | about 20 miles via I-215 South to SR-210 East through Highland, exit San Bernardino Avenue in Redlands, then east to Lugonia Avenue (SR-38), which becomes Mentone Boulevard at Wabash Avenue |
Business lock or door work in Mentone?
Call (951) 903-3193 with the address, the doors or hardware involved and when the site is open. We'll quote the job before any work starts and book a time within our hours that suits your schedule.
Frequently asked questions
Which locks suit washdown or food-processing areas?
Stainless steel levers, sealed or gasketed cylinders and smooth, crevice-free finishes hold up best, because they resist corrosion and clean easily. Lubricants must be ones your sanitation program approves. We choose hardware by the room's cleaning chemicals and temperature, and we schedule installation in a sanitation window so product isn't exposed. Ask your factory locksmith about timing, since a washdown schedule can limit the work window.
How can I check that you're a licensed locksmith?
California licenses locksmith companies through the Bureau of Security and Investigative Services under the Locksmith Act. Our license number is LCO7891, and you can look it up at search.dca.ca.gov before we arrive. Any factory locksmith you hire should give you its legal name and license number when you ask, in writing if you prefer.
Can you open a locked electrical room or chemical cabinet?
Yes, after we verify you have authority over the plant and the escort confirms it's safe to approach. We open with picking or bypass tools where possible, and we won't touch a cabinet that your safety lead says holds hazards we shouldn't handle. For labeled chemical storage, we wait for your authorized person to be present. A cabinet with unknown contents gets a safety check before anyone opens it.
Can you fix exit devices that stick or have been chained?
Yes. We repair, adjust and replace rim, vertical rod and concealed rod exit devices, and we'll remove the cause of a chained door by fitting alarmed hardware or an outside keypad. Exits must open from inside without keys or tools, so we won't make a chain or inside deadbolt permanent. Delayed egress needs fire marshal approval. Quotes always state whether a device is repaired or replaced.
Can you install keypad or card access for restricted areas?
Yes. A factory locksmith can install standalone keypad and card locks and handle the lock and credential side of larger systems. If the door needs power, a network connection or integration with alarms, we coordinate with your electrician or low-voltage contractor. Electronic entry fits labs, prototype rooms and staff doors; low-traffic exterior doors can stay mechanical. We'll mark which doors need power before you commit.
Can you rekey our tool crib and electrical rooms without a shutdown?
In most plants, yes. Rekeying a cylinder takes little time and doesn't touch the equipment inside the room. We schedule it during a break or changeover, test the new key before leaving, and confirm that the door still opens from inside. If a door is in a classified area or needs a permit, we plan that with your safety lead first.
How far is Mentone from your base?
Mentone is about 20 miles from our San Bernardino base, roughly 27 minutes in light traffic. Arrival time depends on traffic and on the job the technician is finishing, so we give you an estimate on the phone before you commit.
Related services in Mentone
- Commercial Locksmith in Mentone
- Industrial Locksmith in Mentone
- Warehouse Locksmith in Mentone
- Key Control System in Mentone
- Employee Key Control System in Mentone
- Restricted Key System in Mentone
- High Security Locksmith in Mentone
- Panic Bar Repair in Mentone
- Commercial Master Key System in Mentone
- Commercial Security Locks in Mentone
Factory Locksmith in nearby cities
- Factory Locksmith in RedlandsSan Bernardino County
- Factory Locksmith in YucaipaSan Bernardino County
- Factory Locksmith in HighlandSan Bernardino County
- Factory Locksmith in Loma LindaSan Bernardino County
- Factory Locksmith in San BernardinoSan Bernardino County
- Factory Locksmith in ColtonSan Bernardino County
- Factory Locksmith in Moreno ValleyRiverside County
- Factory Locksmith in Grand TerraceSan Bernardino County